Laser welding is one of the most precise and flexible processes for joining metallic materials. Thanks to the high energy density of the laser beam, the energy required for welding can be introduced into the workpiece in a highly targeted manner. This results in narrow weld seams, small heat-affected zones and – compared with many conventional welding processes – low thermal distortion.
But which materials can actually be welded with a laser? How much laser power is required, and which type of laser is suitable for the respective application?
The answer does not depend on the material alone. Material thickness, alloy, component geometry, required penetration depth, joint preparation and production speed also play an important role.
Vision Lasertechnik therefore offers a range of laser welding systems and laser sources for manual, semi-automated and fully robot-assisted welding processes.
In general, a wide range of metallic materials can be welded using a laser. Particularly suitable materials include:
Joining dissimilar materials is also possible with certain material combinations. However, particular attention must be paid to the metallurgical properties of both materials.
For this reason, the specific application must always be considered individually.

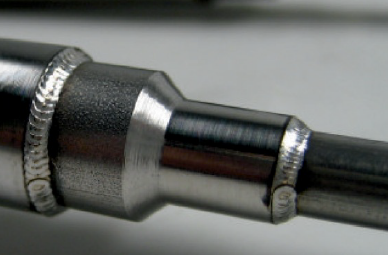
Stainless steel is one of the most commonly laser-welded materials, and many stainless steel alloys offer excellent weldability.
Typical applications can be found in:
One of the key advantages of laser welding stainless steel is the low heat input. This means that even thin-walled or geometrically sensitive components can be joined with minimal distortion.
Depending on the component, both extremely fine weld spots and continuous, gas-tight weld seams can be produced.
Pulsed laser systems are particularly well suited for smaller components, repairs and manual welding applications.
For these applications, Vision offers systems including the T-Base as well as other manual laser welding systems. They provide the operator with highly precise control over the welding process and are suitable for applications such as tool and mould making, precision engineering, and small to medium-sized components.
For higher power requirements and automated processes, Vision uses FSS fibre laser sources.
These are available in different power classes, including:
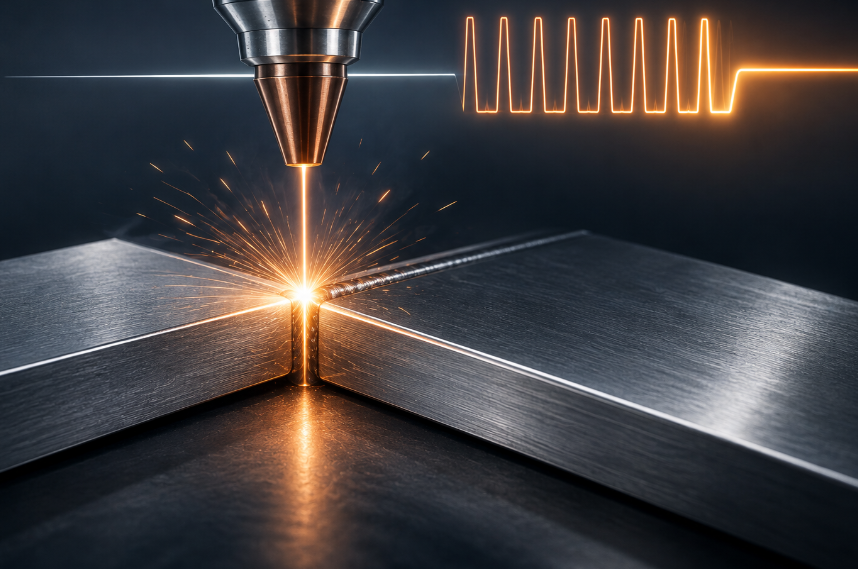
The FSS systems operate in QCW mode (Quasi Continuous Wave), combining high peak pulse power with compact and efficient fibre laser technology.
An FSS laser source with, for example, 300 W average power can achieve peak pulse powers of several kilowatts. This enables a high energy density within the workpiece and therefore greater penetration depths.
For automated applications, these laser sources can, for example, be integrated into our RoboHAWK.
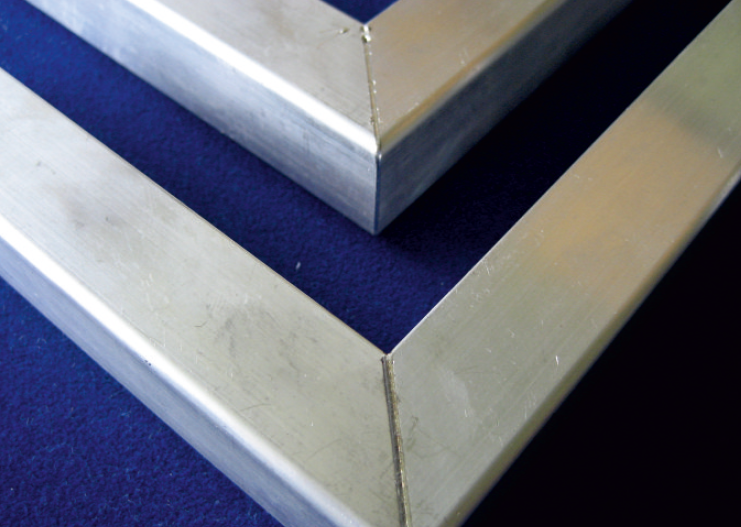
Due to its physical properties, aluminium is more challenging to weld than many types of steel.
The main reasons for this include:
Nevertheless, aluminium can be processed very effectively using suitable laser technology.
Typical applications include:
Laser welding offers particular advantages for thin aluminium components because the energy can be introduced very locally.
Sufficient power reserve is particularly important when welding aluminium.
Depending on material thickness and the specific application, our FSS laser sources with 300 W, 450 W or 600 W can be used, for example.
It is important to understand that the nominal laser power alone does not determine which material thickness can be welded reliably.
Important factors include:
Alloy + material thickness + joint geometry + focal spot diameter + pulse parameters + welding speed + required penetration depth
For critical aluminium components, we therefore generally recommend carrying out a welding trial in our application laboratory.
Unalloyed and low-alloy steels can also be welded using a laser.
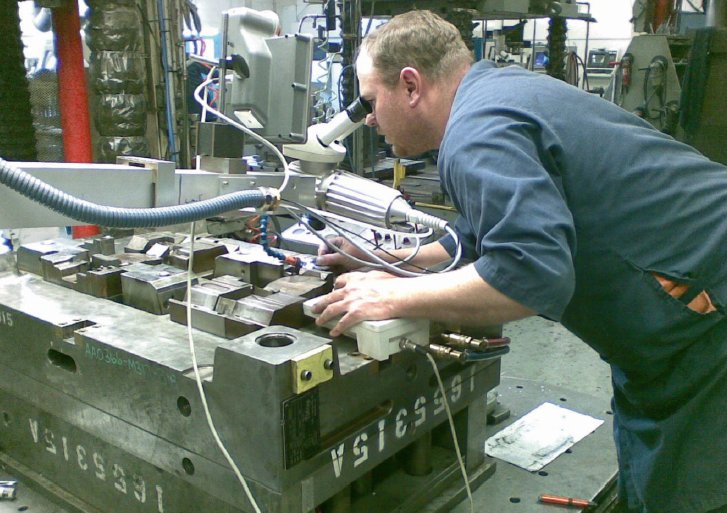
The process is particularly well established in tool and mould making.
Laser welding is used here, for example, to:
A key advantage is that only a very small area of the tool is heated.
This significantly reduces the thermal influence on the surrounding material compared with many conventional welding processes.
Our manual laser welding systems, such as the T-Base, are particularly suitable for these applications.
The operator can precisely observe the welding area through the optical system and apply material exactly where required.
For series-produced components, the same basic process can also be automated. The RoboHAWK with a suitable fibre laser source is an ideal solution for this purpose.
Titanium offers an excellent strength-to-weight ratio and is therefore used in applications including:
Titanium can be laser welded very effectively. However, when heated, the material reacts strongly with oxygen, nitrogen and other components of the ambient air.
Reliable shielding gas coverage is therefore particularly important.
In many applications, argon is used to protect the welding zone from the surrounding atmosphere during the welding process.
With suitable process control, extremely high-quality and precise titanium welds can be produced.
Copper presents a particular challenge for many laser systems.
The main reasons are:
At the same time, laser welding of copper is becoming increasingly important due to electromobility, battery technology and power electronics.
Typical applications include:
Whether an existing fibre laser system is suitable for a specific copper application depends heavily on the material, surface condition, geometry and required penetration depth.
For copper in particular, a decision should therefore not be based solely on the specified laser power.
A practical welding trial often provides significantly more reliable information than a purely theoretical assessment.
Nickel-based alloys are frequently used in applications involving high temperatures, corrosion or high mechanical loads.
Typical applications can be found in:
Many nickel alloys can generally be laser welded effectively. However, the specific process parameters must be adapted to the respective alloy.
Here too, the highly localised heat input of the laser provides advantages when processing sensitive or thin-walled components.
In principle: yes – but not every combination is suitable.
Dissimilar metal welding may, for example, be possible with certain combinations of:
The challenge often lies less in the laser technology itself and more in the metallurgy.
When two different metals come together in the molten weld pool, brittle intermetallic phases, cracks or other undesirable microstructural changes can occur.
The weldability of a dissimilar material joint should therefore always be investigated based on the specific material combination.
A general statement such as “600 W can weld 3 mm stainless steel” is technically only of limited value.
The achievable penetration depth is influenced by numerous factors:
For this reason, we distinguish between the nominal laser power and the welding performance that can actually be achieved within the process.
With QCW laser sources in particular, the high peak pulse power also plays a decisive role.
For many of our modern welding systems, we use FSS fibre laser sources with QCW technology.
QCW stands for Quasi Continuous Wave.
Unlike a conventional CW laser, a QCW source can provide a significantly higher peak power than its specified average power for short periods of time.
This makes it possible to achieve a very high energy density without unnecessarily subjecting the entire component to thermal stress.
This is particularly beneficial for:
Our FSS platform is available in power classes including 150 W, 300 W, 450 W and 600 W.
The most suitable power level depends on the specific application.
The choice of laser system depends not only on the material, but particularly on the production volume, component size, degree of automation and required flexibility.
An initial guideline is shown below:
| Application | Typical System |
|---|---|
| Tool repair | Ergo, WT-Workstation T-Base V3, MobileFlexx |
| Mould making | Ergo, WT-Workstation T-Base V3, MobileFlexx |
| Individual parts | Ergo, WT-Workstation T-Base V3, MobileFlexx |
| Small series | Ergo, T-Base V3, MobileFlexx RoboHAWK |
| Automated series production | RoboHAWK |
| Sensors | Ergo, WT-Workstation T-Base V3, MobileFlexx, RoboHAWK |
| Thermowells | RoboHAWK |
| Membranes | RoboHAWK |
| Complex 3D welding paths | RoboHAWK |
| High process repeatability | RoboHAWK |
For a new application, we therefore do not consider theoretical weldability alone.
What really matters is the actual result on the component.
In our application laboratory, we can investigate questions such as:
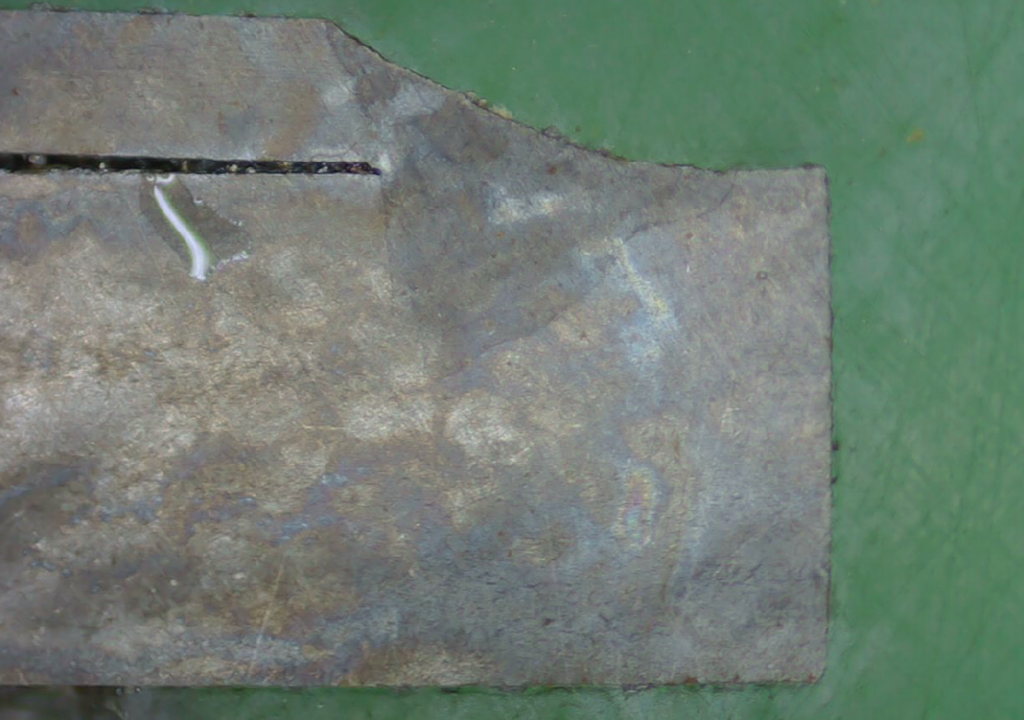
If required, the weld seam can subsequently be examined using a metallographic cross-section analysis. This makes it possible to assess penetration depth, weld geometry, porosity and other characteristics of the joint.
This is particularly important for demanding series-production applications and provides a valuable basis for subsequent process design.
Stainless steel, steel, aluminium, titanium, nickel alloys and many other metals can be laser welded extremely effectively.
The key question is therefore often not:
“Can this material be laser welded?”
but rather:
“Which parameters, laser source and system concept will achieve the best result for this particular component?”
This is precisely where Vision’s expertise comes into play.
We do not simply develop and manufacture laser welding systems. We consider the laser source, optics, workpiece, process, robotics, control system and automation as one integrated system.
From manual laser welding with the T-Base, through our FSS QCW fibre lasers from 150 to 600 W, to the fully automated RoboHAWK, we can adapt the laser technology to the specific manufacturing task.
Would you like to know whether your component can be laser welded?
Send us information about the material and material thickness, a drawing or CAD data and – if available – details of the required production volume and cycle time. We will evaluate your application and, if required, carry out a practical welding trial in our application laboratory.